Get Quick Quote

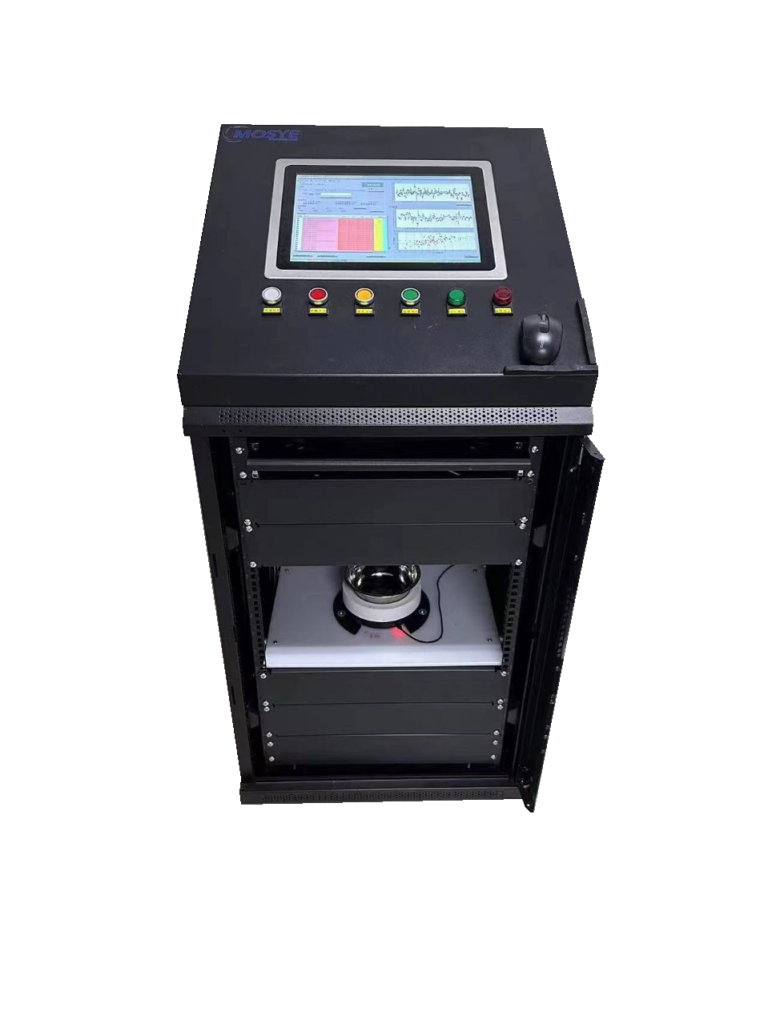
MS-LA-580 Rapid NIR Moisture Analyzer

Direct In-Process Moisture Measurement

The MS-LA-580 provides rapid, non-contact moisture measurement for prepared samples using near-infrared technology.
The integrated system combines the NIR sensor, industrial touch PC, sample-handling system and mobile cabinet, providing an automated testing platform for laboratory and quality-control applications.

Core Information
Detection Target Typical Applications
Moisture Incoming Material Inspection · In-Process Sample Testing · Batch Quality Evaluation · Finished Product Inspection
Product Overview
Rapid Moisture Testing for Quality Control The MS-LA-580 is an integrated NIR analyzer designed for rapid moisture testing of prepared material samples. The automated system measures the sample, displays the result and stores testing data, helping quality-control personnel reduce testing time and manual work. The system can also be configured to evaluate selected organic components, such as protein, fat and total sugar, subject to application evaluation and calibration.
Suitable Process Media
Suitable for selected: Grain and food materials, tobacco materials, ejiao products, chemical and battery materials Supported sample forms include granules, powders, blocks, sheet materials, and selected liquids or slurries. Final suitability depends on the material characteristics, sample form, moisture range, surface condition, and sample-handling requirements.
Measurement Principle
An array of LED sources directs selected near-infrared wavelengths onto the sample surface. Water in the material absorbs part of the NIR energy, while the remaining light is reflected to the optical detector. An application-specific calibration model analyzes the reflected spectral response and converts it into a moisture value.

Key Advantages

1. Rapid Non‑Contact Testing

Measures moisture without direct sensor contact, reducing sample preparation time and material damage during routine testing;

2. Multi‑Spectrum NIR Technology

Uses four groups of NIR LED wavelengths and application‑specific calibration models to evaluate moisture in selected materials;

3. Automated Testing Workflow

Integrates sample measurement, result display, data storage and calibration functions in one quality‑control system;

4. Integrated Industrial System

Combines the NIR sensor, 15‑inch industrial touch PC, sample system and mobile enclosure for convenient laboratory or production‑site use

Technical Specifications

Parameter Specification
Measurement Range 0–100%
Accuracy Up to 0.1%*
Measurement Technology Multi-spectrum near-infrared reflectance
Analog Output 4–20 mA
Communication RS232
Power Supply 100–220 VAC
Analog Input 4–20 mA for PT100 temperature transmitter
Protection Rating IP65
Ambient Temperature −30°C to +60°C

Available Configurations

1
Configuration1

Standard Moisture Testing Configuration: Integrated configuration for rapid moisture testing of selected prepared samples. Includes the NIR measurement unit, touch PC, sample system and mobile enclosure.

2
Configuration2

Application-Specific Sample Configuration: Customized sample holders, testing procedures and calibration models are available for different sample forms and quality-control requirements.

3
Configuration3

Multi-Parameter Analysis Option: Selected applications can be configured to evaluate moisture together with organic components such as protein, fat or total sugar. Available parameters depend on the material and calibration data.

Looking for the Right Solution for Your Application?

Tell us about your material, process conditions or inspection requirements. Our team can help evaluate suitable measurement or quality inspection solutions for your application.