Get Quick Quote

MS-530 Online NIR Composition Analyzer

Direct In-Process Moisture Measurement

The MS-530 provides continuous, non-contact measurement of moisture and selected material components using multi-spectrum LED near-infrared technology.
Designed for conveyors, hoppers, silos and selected process equipment, it provides real-time composition data for process monitoring and quality control.

Core Information
Detection Target Typical Applications
Moisture · Fat · Protein · Fiber · Application-Specific Components Conveyor Belts · Material Transfer Points · Hoppers · Silos · Selected Pipelines · Enclosed Process Equipment
Product Overview
Continuous Composition Measurement Without Sampling Delay The MS-530 uses four groups of near-infrared LED wavelengths to measure reflected spectral information from the material surface. Application-specific calibration models convert the optical response into moisture and selected component values, helping reduce dependence on periodic laboratory sampling. The system integrates local display, parameter setting and data transmission in an industrial die-cast aluminum housing.
Suitable Process Media
The MS-530 can be evaluated for moisture and selected components such as fat, protein and fiber in: Feed and grain materials Starch and food powders Detergent powder Tobacco materials Paper, board and wood products Sinter and selected industrial materials Final capability depends on material characteristics, target component, measurement range, reference method and calibration data.
Measurement Principle
Near-infrared LED light illuminates the material surface. Moisture and other components absorb selected wavelengths differently, producing characteristic reflected spectral responses. The detector collects the reflected light, and an application-specific mathematical model converts the spectral information into the required measurement values.

Key Advantages

1、 Moisture and Composition Measurement Measures moisture

and selected components such as fat, protein and fiber using application‑specific calibration models.

2、 Non‑Contact Online Analysis Measures reflected NIR

signals without direct optical contact, reducing sensor wear and supporting continuous production monitoring.

3、 Stable Industrial Measurement Signal processing helps

reduce the influence of material colour variation, ambient light and changing surface conditions.

4、 Flexible Installation and Integration Supports standard

or insertion‑mounted configurations, air purging, analog outputs, RS232/RS485 communication and external measurement control.

Technical Specifications

Parameter Specification
Measurement Technology Multi-spectrum LED NIR
Moisture Range 0–90%, application-dependent
Accuracy Up to 0.1%, application-dependent
Light Source Four groups of NIR LED wavelengths
Wavelength Range 940–1550 nm
Available Models MS-530-S standard / MS-530-M insertion-mounted
Analog Output 2 × 0/4–20 mA
Communication RS232 / RS485
Power Supply 24 VDC; 220 VAC optional
Ambient Temperature −20°C to +85°C
Storage Temperature −30°C to +95°C
Air Purging Integrated purge connection

Available Configurations

1
Configuration1

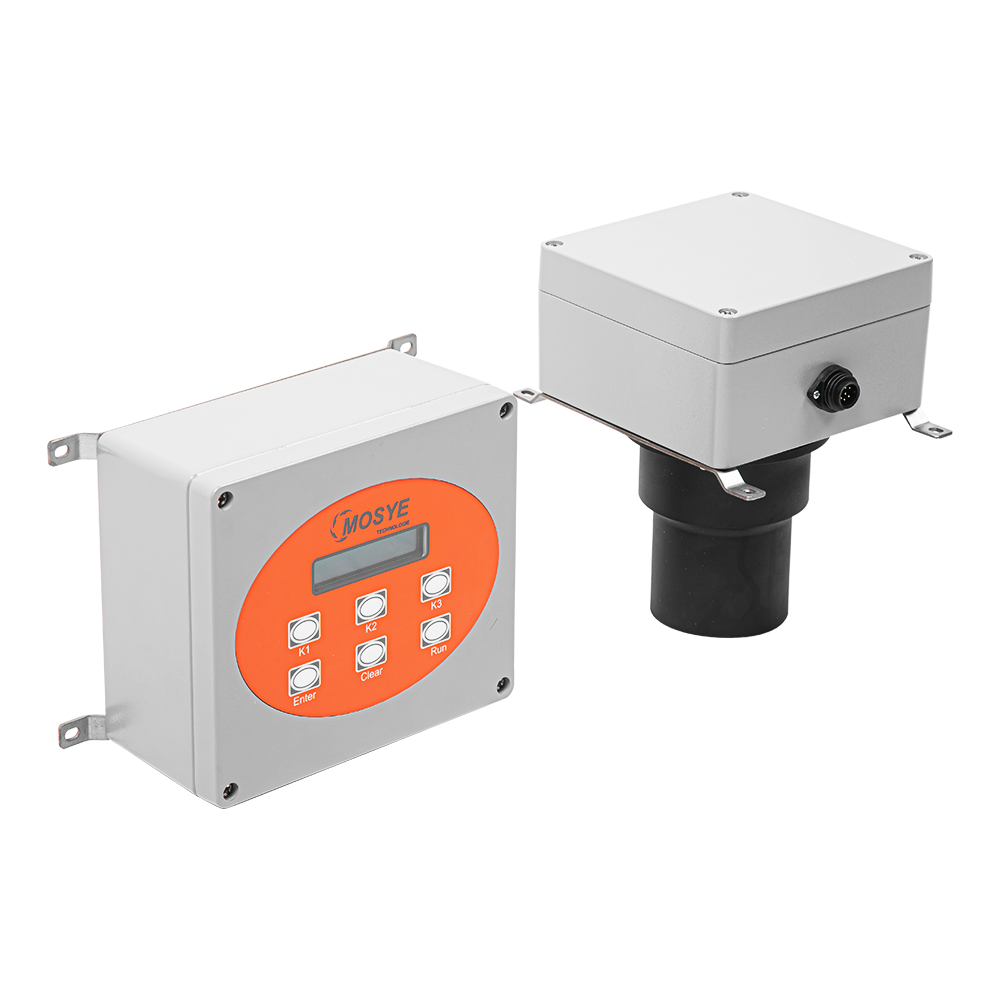
MS-530-S — Standard Configuration: Non-contact optical configuration for installation above open material surfaces. Typical installations include: Conveyor belts \Material transfer points \Open production lines \Surface-composition measurement

2
Configuration2

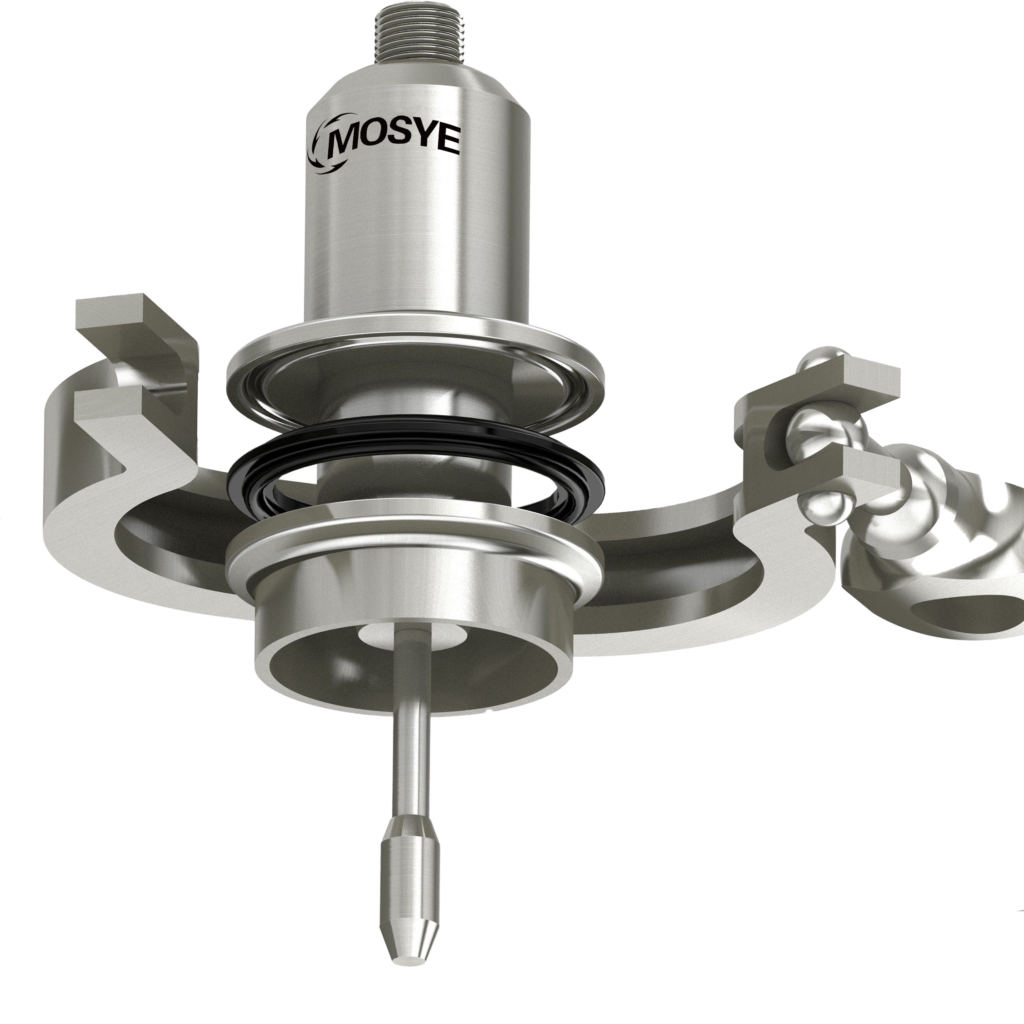
MS-530-M — Insertion-Mounted Configuration: Optical probe designed for selected hoppers, silos, pipelines and enclosed process equipment. The probe extends into the material area while measurement is performed optically at the sensor window. Final suitability depends on material visibility, buildup, dust and cleaning requirements.

Looking for the Right Solution for Your Application?

Tell us about your material, process conditions or inspection requirements. Our team can help evaluate suitable measurement or quality inspection solutions for your application.